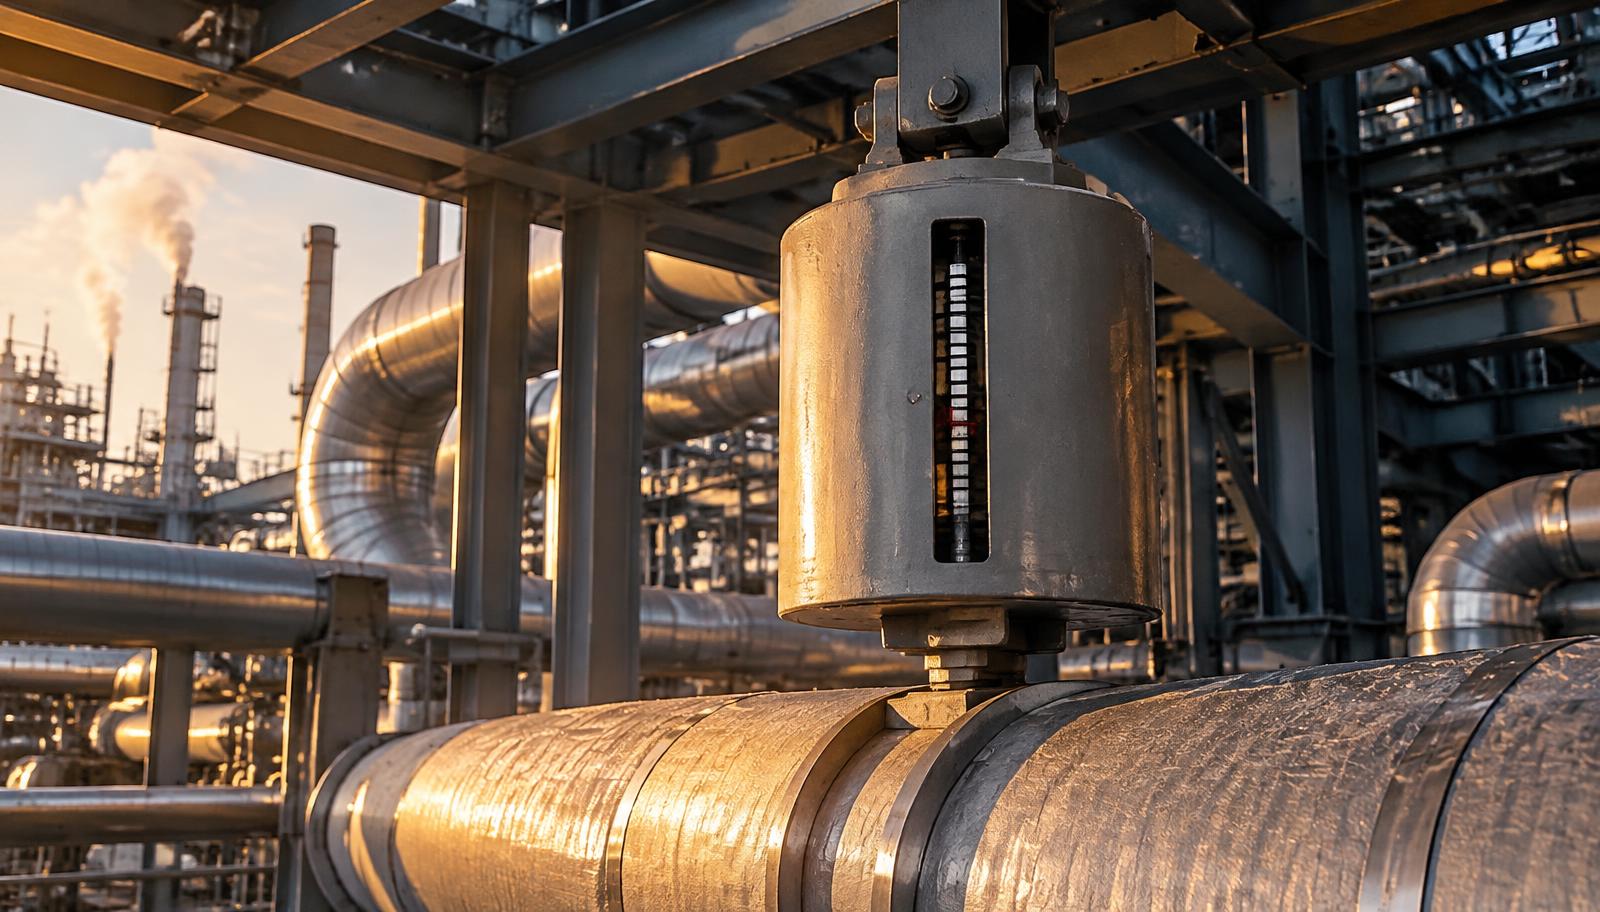
A spring hanger is not hardware. It is a calibrated boundary condition in the piping system's load path and thermal-movement strategy. When it is selected wrong, set wrong, left blocked, packed with debris, corroded or adjusted without analysis, it stops behaving like a spring and starts behaving like an anchor. The load does not disappear. It migrates into welds, flanges, branch connections and the nozzles of the pumps, compressors and turbines the piping was designed to protect. This article sets out how BlackOut Power Group approaches spring supports from stress model to turnaround, and how an owner can manage hundreds or thousands of them as a governed asset population rather than as anonymous steel.
01
The spring hanger as an active boundary condition
Piping grows when it heats. Where that growth has a vertical component, a rigid support either lifts off and stops carrying weight, or holds the pipe and resists the growth. Neither is acceptable near sensitive equipment. A spring support solves the problem by carrying weight while permitting calibrated vertical movement.
The analysis that sized the spring assumed a stiffness. When a spring bottoms out, tops out, seizes, or is left pinned, its effective stiffness jumps by orders of magnitude. The boundary condition changes, the stiffness matrix of the system changes, and the reactions redistribute. A spring problem does not stay at the spring.
- Thermal-growth loads redirected into the nearest rigid restraint or equipment nozzle.
- Deadweight dumped onto adjacent supports when a spring tops out or a shoe lifts off.
- Shifted natural frequencies and mode shapes that can bring a span toward an excitation frequency.
- Cyclic bending at welds, branch connections and small-bore fittings.
- Flange rotation and loss of gasket stress on one quadrant, producing leaks at temperature.
The indicator on the spring is not decoration. It is one of the few places where the piping stress analysis becomes directly visible in the field.
02
Support taxonomy: functions that are routinely confused
Many field problems begin with a misunderstanding of what a support is supposed to do. A guide is not a restraint for weight. A snubber is not a spring. A rigid rod hanger adjacent to a spring takes everything the spring gives up. Inspectors and planners should know the intended function before they judge the condition.
| Support | Intended function | Typical failure signature |
|---|---|---|
| Rigid hanger / rest | Carries weight with no vertical travel | Lift-off when hot; overload when an adjacent spring fails |
| Variable spring | Carries weight; load changes linearly with travel | Topped out, bottomed out, wrong setting, coil bind |
| Constant support | Carries substantially uniform load through travel | Seized linkage, pivot wear, travel at scale limits |
| Snubber (hydraulic / mechanical) | Free for slow thermal movement; resists dynamic events | Fluid loss, seized mechanism, locked against thermal growth |
| Sway brace | Light spring restraint against low-amplitude vibration | Over-preload, misadjustment, bent rod |
| Guide | Permits axial movement; restrains lateral | Binding, missing gap, worn slide surface |
| Anchor / restraint | Fixes movement in defined directions | Cracked attachment welds, structural distortion |
03
Variable spring arrangements
Variable springs are supplied in standard physical arrangements that differ by how the canister connects to structure and pipe. Manufacturers commonly designate these as Types A through G. Nomenclature varies by supplier, so the hanger schedule and manufacturer drawing, not a generic letter, define what is installed.
| Type | Arrangement | Typical use |
|---|---|---|
| A | Threaded top connection, suspended | Rod-hung from overhead steel directly above the pipe |
| B / C | Single or double lug top attachment | Pin or clevis connection to structural attachment above |
| D / E | Canister resting on steel, rod passing through | Limited headroom; canister sits on beams with rod through the gap |
| F | Base-mounted with load column | Pipe or equipment supported from below; needs lateral stability and often a slide plate |
| G | Trapeze, paired canisters on a cross-member | Large pipe, twin lines, or where a single rod is obstructed |
04
Engineering mechanics: variable versus constant
A variable spring follows Hooke's law. Its support force changes by ΔF = k·Δy as the pipe moves, where k is the spring rate and Δy the vertical travel. The design objective is that the spring carries the calculated operating load in the hot, steady-state position, so the analysis assumption holds when the plant is running. The cold, installed load is back-calculated from that hot load. For pipe moving up, the spring extends and its force falls: F_cold = F_hot + k·Δy. For pipe moving down, the spring compresses further: F_cold = F_hot − k·|Δy|.
Load variability, |F_hot − F_cold| divided by F_hot, measures how much load the spring sheds or picks up between conditions. MSS SP-58 and ASME B31.1 practice typically limit variable spring variability to 25 percent. That limit is a ceiling, not a target. Lines connected to rotating equipment frequently need tighter values, and many owner specifications set lower limits or require constant supports near machinery nozzles, because the load the spring sheds is load the nozzle receives.
A constant support uses a lever, cam or linkage so the moment produced by the spring balances the pipe load throughout travel. ASME B31.1 and MSS SP-58 typically limit the load deviation of constant supports to about 6 percent across the working range. Constant supports are selected where travel is large, where variability would be excessive, or where high-temperature critical service and nozzle sensitivity make load change unacceptable. They cost more, weigh more, and carry mechanisms that need inspection.
Load versus travel: three support behaviors
- 01
Rigid support
Zero travel. Either carries the load or lifts off. Takes everything an adjacent failed spring gives up.
- 02
Variable spring
Load changes linearly with travel, ΔF = k·Δy. Set to carry the operating load hot; variability typically limited to 25 percent, tighter near machinery.
- 03
Constant support
Linkage balances spring moment against pipe load. Load deviation typically held to about 6 percent through the working range.
- 04
Bottomed or pinned spring
Effective stiffness becomes rigid. Thermal growth is resisted and load migrates to nozzles and restraints.
05
The sizing sequence: from stress model to hardware
Spring selection is not a catalog exercise. It begins in the piping flexibility model, where sustained, operating, occasional and hydrotest cases establish loads and movements, and it ends with a manufacturer selection that fits real hardware into real geometry.
- 1. Model the system in Hexagon CAESAR II or Bentley AutoPIPE with correct weights, including insulation, valves, actuators and contents.
- 2. Run the hanger design algorithm to establish operating load and vertical travel at each spring location, with adjacent restraints active.
- 3. Add travel margin so the working range never reaches the casing limits; owner specifications commonly require margin above calculated travel at both ends.
- 4. Select spring size from load and spring range from travel; check variability against the governing limit and the connected equipment.
- 5. If variability or nozzle load is unacceptable, use a longer-range spring with a lower rate, or a constant support.
- 6. Check the hydrotest case. Water-filled vapor or steam lines can weigh several times their operating weight; specify travel stops or temporary supports rated for it.
- 7. Complete the selection in manufacturer engineering software such as LISEGA LICAD or the supplier's equivalent: hardware, rods, clamps, clamp material for temperature, clearances, and the cold and hot settings on the travel scale.
| Question | Primary tool | What it produces |
|---|---|---|
| How will the system move and what loads result? | Hexagon CAESAR II / Bentley AutoPIPE | Displacements, support reactions, nozzle loads, spring loads and travel |
| Which real support satisfies that load and travel? | LISEGA LICAD / manufacturer selection engineering | Selected variable or constant support, hardware, drawings, settings |
| Is a local or dynamic effect beyond beam-model scope? | ANSYS Mechanical | Local stresses at lugs and trunnions, nonlinear contact, modal results |
| Is connected machinery affected? | Bently Nevada System 1 / ADRE, Emerson AMS Machinery Manager | Vibration signatures, casing and alignment indications |
06
Hydrotest and travel stops: the commissioning hazards
Springs are shipped with travel stops that lock them at the cold setting. They protect the spring during erection and carry hydrotest weight. Two opposite errors follow. If stops are removed before hydrotest, the water weight can drive the spring toward solid height, overload structure, and permanently change the spring. If stops are left in after hydrotest, the spring becomes a rigid support, and the first heat-up forces thermal growth against it.
Every travel stop should be tagged, listed on the punchlist, verified engaged before filling, and verified removed, by name and with a photograph, before warm-up. Startup should not proceed with any stop unaccounted for.
07
Cold walk and hot walk: reading the stress model in the field
The travel scale marks the design cold and hot positions. A cold walk before startup records the actual cold position, travel-stop status, rod alignment and hardware condition. A hot walk at stable operating temperature records the actual hot position, remaining travel and the behavior of adjacent supports. The comparison of design cold, actual cold, design hot and actual hot is the most useful single record a plant can keep on a spring.
Rod angularity matters. MSS SP-58 practice commonly limits rod swing to about 4 degrees from vertical. Beyond that, a rod hanger applies an unintended lateral force and bends at the threads, where fatigue resistance is lowest. Where horizontal movement is significant, the designer may offset the rod cold so it is near vertical hot, or use a roller or slide arrangement.
Reading the travel scale
- 01
Design cold
Calculated installed position, marked on the scale at fabrication.
- 02
Actual cold
Recorded before startup with every travel stop confirmed removed.
- 03
Design hot
Calculated operating position where the spring carries the operating load.
- 04
Actual hot
Recorded at stable operating temperature; compared against design and trended over years.
- 05
Reserve travel
Remaining movement before topping or bottoming. Loss of reserve is an investigation trigger.
- 06
Travel stop
Tagged, engaged for hydrotest, removed and photographed before warm-up.
| Field | Design | Actual | Status |
|---|---|---|---|
| Hanger ID | SH-101 | SH-101 | Confirmed |
| Cold position (scale) | 3.2 | 3.3 | Accept |
| Hot position (scale) | 6.1 | 5.0 | Investigate |
| Reserve travel at hot | Within working range | Near top limit | Investigate |
| Travel stop | Removed | Removed | Accept |
| Rod angle hot | Under 4° | 6° | Investigate |
| Corrosion | None expected | Moderate on rod threads | Repair |
| Adjacent support | Shoe in contact | Shoe lifted | Investigate |
08
When the indicator is wrong: investigate before adjusting
The common field reaction to an out-of-position indicator is to turn the turnbuckle until the pointer looks right. That jacks the pipe. It imposes a displacement the analysis did not include and moves load to the nearest restraint or nozzle. The indicator is reporting the equilibrium of the system; the question is why that equilibrium changed.
- Confirm line condition: truly at steady operating temperature, pressure and flow, not mid-transient.
- Check the design settings on the current hanger schedule, not an old drawing.
- Check for travel stops, interference, rubbing or contact with structure.
- Inspect rods, turnbuckles, clamps and attachments for bending, slippage or cracking.
- Check adjacent supports for lift-off, binding or failure that has shifted load.
- Check for weight changes: insulation replacement, wet insulation, added valves, actuators or tie-ins.
- Check for structural settlement and modified guides or anchors.
- Review the stress model; measure loads or movements where needed.
- Determine the cause, then engineer the adjustment, rebalancing or replacement.
- Verify the result in both cold and hot conditions.
09
Machinery, nozzle loads and dynamic behavior
A spring hanger does not create excitation. Unbalance, misalignment, flow pulsation and vane-pass forces do. What a failed or seized support changes is the system: static loads on the nozzle, and the stiffness that sets natural frequencies, which for a simplified system scale with the square root of stiffness over mass. A bottomed spring or rigid contact can raise a span's frequency toward a running-speed or pulsation frequency.
Nozzle loads at pumps, compressors and steam turbines are limited by API 610, API 617, NEMA SM 23 and OEM data. Loads above those limits can distort casings and move bearings and seals off their intended alignment. The defensible statement is that incorrect support behavior can alter the static and dynamic load path and may contribute to vibration, misalignment, seal and bearing distress, or fatigue. Causation requires evidence: travel data, stress results and vibration data from platforms such as Bently Nevada System 1 or Emerson AMS Machinery Manager.
How a support problem reaches the machine
- 01
Spring bottoms, tops out or seizes
Support stiffness and load no longer match the analysis.
- 02
Load redistributes
Adjacent supports lift off or overload; thermal growth is restrained.
- 03
Nozzle forces and moments rise
Loads approach or exceed API 610, API 617, NEMA SM 23 or OEM limits.
- 04
Casing and alignment shift
Bearing, seal and coupling alignment move from the intended condition.
- 05
Symptoms appear
Vibration, seal leakage, bearing temperature, flange leaks or fatigue cracking.
10
Environment: debris, corrosion, lubrication and cleaning
Spring supports sit in dust, rain, salt, chemical vapor and heat. Fly ash, coal dust, catalyst fines, blast grit and insulation debris collect in canister openings and between coils. Packed debris reduces free travel, so a spring can become coil-bound before reaching its design position. Water trapped in a canister with blocked drain openings keeps the lower coils and guide plate wet, accelerating corrosion. Pitting on high-strength spring wire is a fatigue initiation site. Seized turnbuckle threads make correct adjustment impossible when it is finally needed.
Lubrication must follow the manufacturer's instruction, nothing more. Helical coils have no sliding surfaces and should not be greased; grease holds grit. PTFE slide plates on base supports are designed to run dry; grease, oil or paint degrades them and raises friction. Some constant-support pivots and bearings use self-lubricating bushings; others call for a specified lubricant at a specified interval. Do not lubricate a support simply because it moves.
Environmental degradation at the support
- 01
Packed debris
Ash, dust or catalyst fines between coils reduce free travel and cause coil bind.
- 02
Blocked drains
Standing water corrodes the lower coil, guide plate and canister base.
- 03
Wire and thread corrosion
Pitting initiates fatigue; seized turnbuckles prevent correct adjustment.
- 04
Rod angularity
Swing beyond about 4 degrees adds lateral load and bends the rod at the threads.
- 05
Retained travel stop
A pinned spring behaves as a rigid support at first heat-up.
- 06
Contaminated slide plate
Grease or grit on PTFE raises friction and restrains horizontal movement.
| Condition | Effect | Inspection and maintenance response |
|---|---|---|
| Dust, ash, catalyst fines between coils | Reduced free travel; coil bind | Dry removal with low-pressure air or soft brush; record before and after |
| Blocked drain openings | Standing water; accelerated corrosion | Clear drains; check canister base and lower coil |
| Coastal / chemical atmosphere | Pitting of wire, rods and pins; seized threads | Coating condition per ISO 12944 category; thread condition; replace where pitting is significant |
| Grease on coils or PTFE | Grit retention; raised friction | Remove per manufacturer guidance; correct the procedure that applied it |
| Washdown or blasting | Grit forced into mechanism; scale markings lost | Protect supports; avoid high-pressure jets; re-mark scales from the hanger schedule |
| Heat from uninsulated surfaces | Spring and clamp temperature above rating | Confirm clamp material and spring location against temperature limits |
11
Inspection frequency and type by support
A uniform interval for every spring is not a strategy. Frequency should follow consequence, movement, cycling, environment, proximity to machinery and history. The structure below is a typical starting point; criticality and FMECA should then adjust it per population.
- Variable springs: indicator position, reserve travel, coil condition, debris, drains, rods and turnbuckles.
- Constant supports: position within the working scale, linkage and pivot condition, lubrication only if specified, structural attachment.
- Hydraulic snubbers: fluid level, leakage, rod condition, freedom for thermal movement; functional testing per program.
- Mechanical snubbers: freedom of slow movement, no drag or lock-up, attachment condition.
- Rigid hangers and guides: contact, lift-off, gaps, wear and binding.
| Tier | When | Scope | Applies to |
|---|---|---|---|
| Operator observation | Routine rounds | Indicator within range, no topping or bottoming, no visible stops, rods not cocked, no rubbing | All springs and constants on accessible lines |
| Cold walk | Before every startup after outage | Cold position, travel stops removed, rod angle, hardware, corrosion, drains | All springs; constants and snubbers |
| Hot walk | At stable operating condition after startup and periodically | Hot position, reserve travel, adjacent supports, interference, vibration | All springs; priority on high-energy and machinery-connected lines |
| Turnaround inspection | Major outage | Attachment welds (MT/PT where warranted), UT of corroded parts, pins and linkages, load verification where justified | High-criticality populations, constants, snubbers |
| Engineering reassessment | After MOC, recurring deviation or failure | Stress model review, rebalancing, replacement design | Affected line |
12
Replacement and rebalancing
Replacing a failed spring with the same catalog number may reproduce the original error if the system has changed. Before replacement, confirm the design basis: current insulation, valves, contents, temperature and adjacent support condition. Where any of these changed, re-analyze. Where one spring is out, its neighbors are often out too; rebalancing may involve several supports. Install with stops engaged, set to the calculated cold position, remove stops under control, and verify cold and hot.
Spares strategy follows the installed base. Identify critical assemblies, long-lead constant supports, model standardization across units, and what parts are replaceable versus whole-assembly. Inventory belongs in SAP or Maximo; the consequence logic that decides what to stock comes from criticality and FMECA review.
13
The digital travel sheet: lifecycle traceability with QC Lite
Most plants hold spring data in five disconnected places: the stress report, vendor drawings, hydrotest punchlists, commissioning notebooks and operator logs. When an indicator drifts years later, nobody can tell whether it was set wrong, adjusted during a turnaround, or whether the line has migrated.
BPG QC Lite, a digital quality platform under development at BlackOut Power Group, is designed to carry each spring as a serialized record on a signed digital travel sheet through every stage of its life. Each gate records the required readings and photographs, names who performed and who accepted the step, and holds the next step until the current one is signed. The platform supports the process; the Responsible Engineer and the owner's procedures govern acceptance.
Program governance and the signed travel sheet
- 01
Policy and ownership
Site standard adopting MSS SP-58 and ASME B31; named program owner and Responsible Engineer.
- 02
Register and criticality
Every support in SAP or Maximo; populations tiered with BPG Criticality.
- 03
Strategy
BPG FMECA sets failure modes, detection and inspection tiers.
- 04
Travel sheet gates
Receipt, installation, hydrotest hold, cold and hot commissioning, surveillance, turnaround disposition.
- 05
Competency and MOC
Role-based qualification; insulation, valve and routing changes trigger support review.
- 06
Audit and trend
Percentage in tolerance, open deviations, stops unaccounted, recurring offenders.
| Gate | Recorded evidence | Sign-off |
|---|---|---|
| 1. Receipt | Tag, model, range, rate, cold and hot loads against schedule; stops installed; photographs | Receiving inspector |
| 2. Installation | Attachment, rod angle, clamp, insulation clearance, initial position | Installer and QC inspector |
| 3. Hydrotest hold point | Stops engaged or temporary supports in place; post-drain confirmation | QC inspector and test lead |
| 4. Cold commissioning | Every stop removed and accounted for; actual cold versus design cold | QC inspector and operations |
| 5. Hot commissioning | Actual hot versus design hot; reserve travel; adjacent supports | Piping engineer and operations |
| 6. Surveillance | Periodic readings trended over years; deviation flags | Inspector; engineer on deviation |
| 7. Turnaround and disposition | NDE results, repairs, engineering disposition before any adjustment | Responsible Engineer |
14
Building a Spring Hanger Integrity Program
Owners run formal programs for pressure equipment, relief devices and rotating machinery. Spring supports deserve the same: a Spring Hanger Integrity Program that sits within the asset integrity management system and makes the rules above enforceable, trained and auditable. Without it, the knowledge lives with one stress engineer and a few experienced millwrights, and it leaves when they do.
- Policy: a site or corporate standard adopting MSS SP-58 and the applicable ASME B31 code, naming the program owner and the Responsible Engineer for piping supports.
- Register: every spring, constant and snubber tagged by line and location in SAP S/4HANA Asset Management or IBM Maximo, with design data and documents attached.
- Criticality: populations ranked with BPG Criticality using line consequence, temperature, connected machinery, travel and history, to set inspection tiers. Criticality ranks attention; it does not size springs.
- Failure-mode strategy: BPG FMECA covering coil failure, corrosion, seizure, retained stops, topping and bottoming, wrong setting, misalignment and attachment cracking, with detection methods and intervals.
- Procedures: travel-stop control, cold and hot walk instructions, investigate-before-adjust, lubrication and cleaning rules, replacement and rebalancing.
- Competency: role-based qualification for operators, technicians, turnaround contractors and engineers, refreshed periodically.
- Management of change: insulation, valve or actuator changes, reroutes, tie-ins and temperature or service changes trigger a support review.
- Records: stress models, isometrics, hanger schedules, datasheets and survey history reconciled in the engineering document system, with BPG Engineering Records Intelligence supporting reconciliation where records disagree.
- Audit and improvement: percentage of springs in tolerance, open deviations, stops unaccounted at startup, and recurring offenders reported to management.
| Role | Responsibility | Competency expected |
|---|---|---|
| Operator | Observe indicators, stops, cocked rods, rubbing; report | Recognize abnormal positions and visible damage |
| Maintenance technician | Execute walkdowns, record readings, clean, inspect hardware | Read scales, measure rod angle, apply cleaning and lubrication rules |
| Turnaround / piping contractor | Install, pin and unpin springs, replace hardware | Travel-stop control, setting procedure, no unauthorized adjustment |
| Inspector / QC | Witness gates, verify evidence, raise deviations | Code and procedure acceptance criteria, NDE referral |
| Responsible piping engineer | Disposition deviations, authorize adjustment and replacement, own the model | Flexibility analysis, spring selection, machinery interface |
15
The do's and don'ts every site should publish
Rules that are not written down and trained are not rules. The following belong on the first page of the procedure and in every contractor induction for outage work on piping.
| Rule | Reason |
|---|---|
| Do not adjust a turnbuckle to correct an indicator without engineering disposition | The indicator reports system equilibrium; adjusting it jacks the pipe |
| Do verify every travel stop removed before warm-up | A pinned spring is a rigid support against thermal growth |
| Do keep stops engaged or temporary supports in place for hydrotest | Water weight can exceed spring range and structure ratings |
| Do not grease coils or PTFE slide surfaces | Grease holds grit, causes coil bind and raises friction |
| Do keep drain openings clear and remove debris dry | Standing water and packed debris drive corrosion and lost travel |
| Do record cold and hot readings against the current schedule | Trends reveal migration, settlement and load changes |
| Do not replace like-for-like without confirming the design basis | A changed system makes the original selection wrong |
| Do raise an MOC review for insulation, valve or routing changes | Weight and stiffness changes invalidate spring settings |
16
Toolchain by lifecycle stage
Each tool answers one question. The value lies in the handoffs: the stress model sets the requirement, the manufacturer selection meets it, the field record confirms it, and the maintenance system keeps it confirmed. BPG professionals work in the client's established platforms; the tools named are industry-standard examples, and equivalent systems can fill the same roles.
| Engineering question | Primary tool | Supporting layer |
|---|---|---|
| How much will the pipe move, and what loads result? | Hexagon CAESAR II | Bentley AutoPIPE |
| Which variable or constant support should be selected? | LISEGA LICAD / manufacturer engineering | Supplier catalogs and drawings |
| Are local or dynamic effects beyond beam-model scope? | ANSYS Mechanical | CAESAR II dynamic analysis |
| Is connected machinery affected? | Bently Nevada System 1 / ADRE | Emerson AMS Machinery Manager |
| Is the hanger in the correct hot and cold position? | Calibrated travel-scale reading and dimensional survey | Digital inclinometer; laser survey where justified |
| Which populations deserve the most attention? | BPG Criticality | Client criticality method in SAP or Maximo |
| Which failure modes must maintenance manage? | BPG FMECA | SAP APM where the client operates it |
| Which spares should be stocked? | SAP S/4HANA / IBM Maximo inventory | BPG Criticality and FMECA review |
| How is lifecycle evidence captured and signed? | BPG QC Lite (in development) | Client inspection or CMMS records |
| How are design and history reconciled? | Engineering document system | BPG Engineering Records Intelligence |
17
Design it. Set it. Observe it. Trend it. Investigate before adjusting it.
A spring hanger performs a simple-looking job inside a complex system: carry the intended load while allowing the intended movement. When either half of that function is lost, the consequence appears somewhere else, at another support, a flange, a weld, a branch connection or a machine nozzle.
Organizations that treat spring supports as an asset population, with a register, a criticality-based strategy, trained people, controlled procedures and a signed record of every reading, find these problems while they are still positions on a scale rather than cracks, leaks and trips.
Related Capability
Continue Reading
- It's Not Just a Gasket: Eliminating Flange Leaks Through Bolted Joint Engineering, Controlled Bolting, and Assembly Governance
Pressure Systems
- Criticality Is Not Priority: How Engineering Leaders Decide What Work Comes First
Asset Advisory
- Engineering the Unbreakable Train: A Quantitative FMECA for Coupled Turbine, Expander & Compressor Assets
Machinery Diagnostics
Technical References
Standards basis and scope references.
- 01 MSS SP-58, Pipe Hangers and Supports: Materials, Design, Manufacture, Selection, Application, and Installation. Current editions consolidate content formerly published in MSS SP-69 and SP-89; confirm the edition adopted by the project.
- 02 ASME B31.1 Power Piping, including requirements for variable and constant spring supports, load variation and travel indication.
- 03 ASME B31.3 Process Piping, including support and restraint design and flexibility analysis requirements.
- 04 API 610 (centrifugal pumps), API 617 (centrifugal compressors) and NEMA SM 23 (steam turbines) for allowable nozzle loads, together with OEM-specific limits.
- 05 API 570 for in-service inspection of piping systems, including supports, where adopted by the owner.
- 06 ISO 12944 for atmospheric corrosivity categories and protective coating selection.
- 07 Manufacturer installation, operation and maintenance manuals govern setting, travel-stop removal, lubrication and adjustment of specific products.
- 08 Numerical limits shown are typical code and industry values for discussion. The adopted code edition, owner specification, stress analysis and manufacturer data govern. Example readings are illustrative.
Applicability and adopted editions must be confirmed against the governing contract, authority, location, cable construction, and manufacturer requirements.